Operational Efficiency: How the CMR1000A Defeats the "Changeover Downtime" on Dual-Purpose Rigs
If you browse through hands-on threads on r/mining or r/Geotech, you will find that field drillers and offsiders harbor a healthy skepticism toward multi-functional drilling rigs. The common complaint isn't about the theoretical specs on paper; it's about the brutal reality of the site changeover.
As one Reddit user bluntly put it: “Sure, a hybrid rig sounds great to the accountants in the city. But when you are out in 40°C heat in a remote desert, trying to manually swap out heavy breakout jaws, sub-adapters, and mud lines to switch from RC to core, the downtime eats all your simulated profits.”
This is a valid criticism. In exploration, time is literally money. If a combination rig takes a full shift or two just to transition from Reverse Circulation (RC) overburden pre-collaring to diamond wireline coring, its utilization rate plummets.
Today, we look under the hood of the CMR1000A Multi-Functional Combination Drilling Rig—engineered by JINNENG HOLDING EQUIPMENT MANUFACTURING GROUP—to explore how smart mechanical integration minimizes operational complexity for the field crew.
The Root Cause of Changeover Fatigue
On traditional or poorly designed hybrid rigs, switching from RC to Diamond Core drilling requires intensive manual labor:1.Breaking Down the RC String: Stripping the heavy, dual-wall RC rods, removing the air hammer, and disconnecting the heavy-duty cyclone hoses.
2.Modifying the Head and Floor: Manually changing the rotation head sub-adapters to handle coring strings, and swapping the slips, chuck jaws, and manual breakout wrenches at the foot clamp.
3.Fluid System Re-routing: Manually closing high-pressure air valves from the auxiliary compressor and re-plumbing the high-pressure coring mud pumps.
For a two- or three-man crew, this is backbreaking work that invites high injury risks and massive operational downtime.
The CMR1000A Solution: Engineered Floor Automation
The engineering team behind the CMR1000A engineered out this complexity by designing a fully integrated, multi-compatible automated lower mast floor.1. Integrated Dual-Compatible Hole Tools
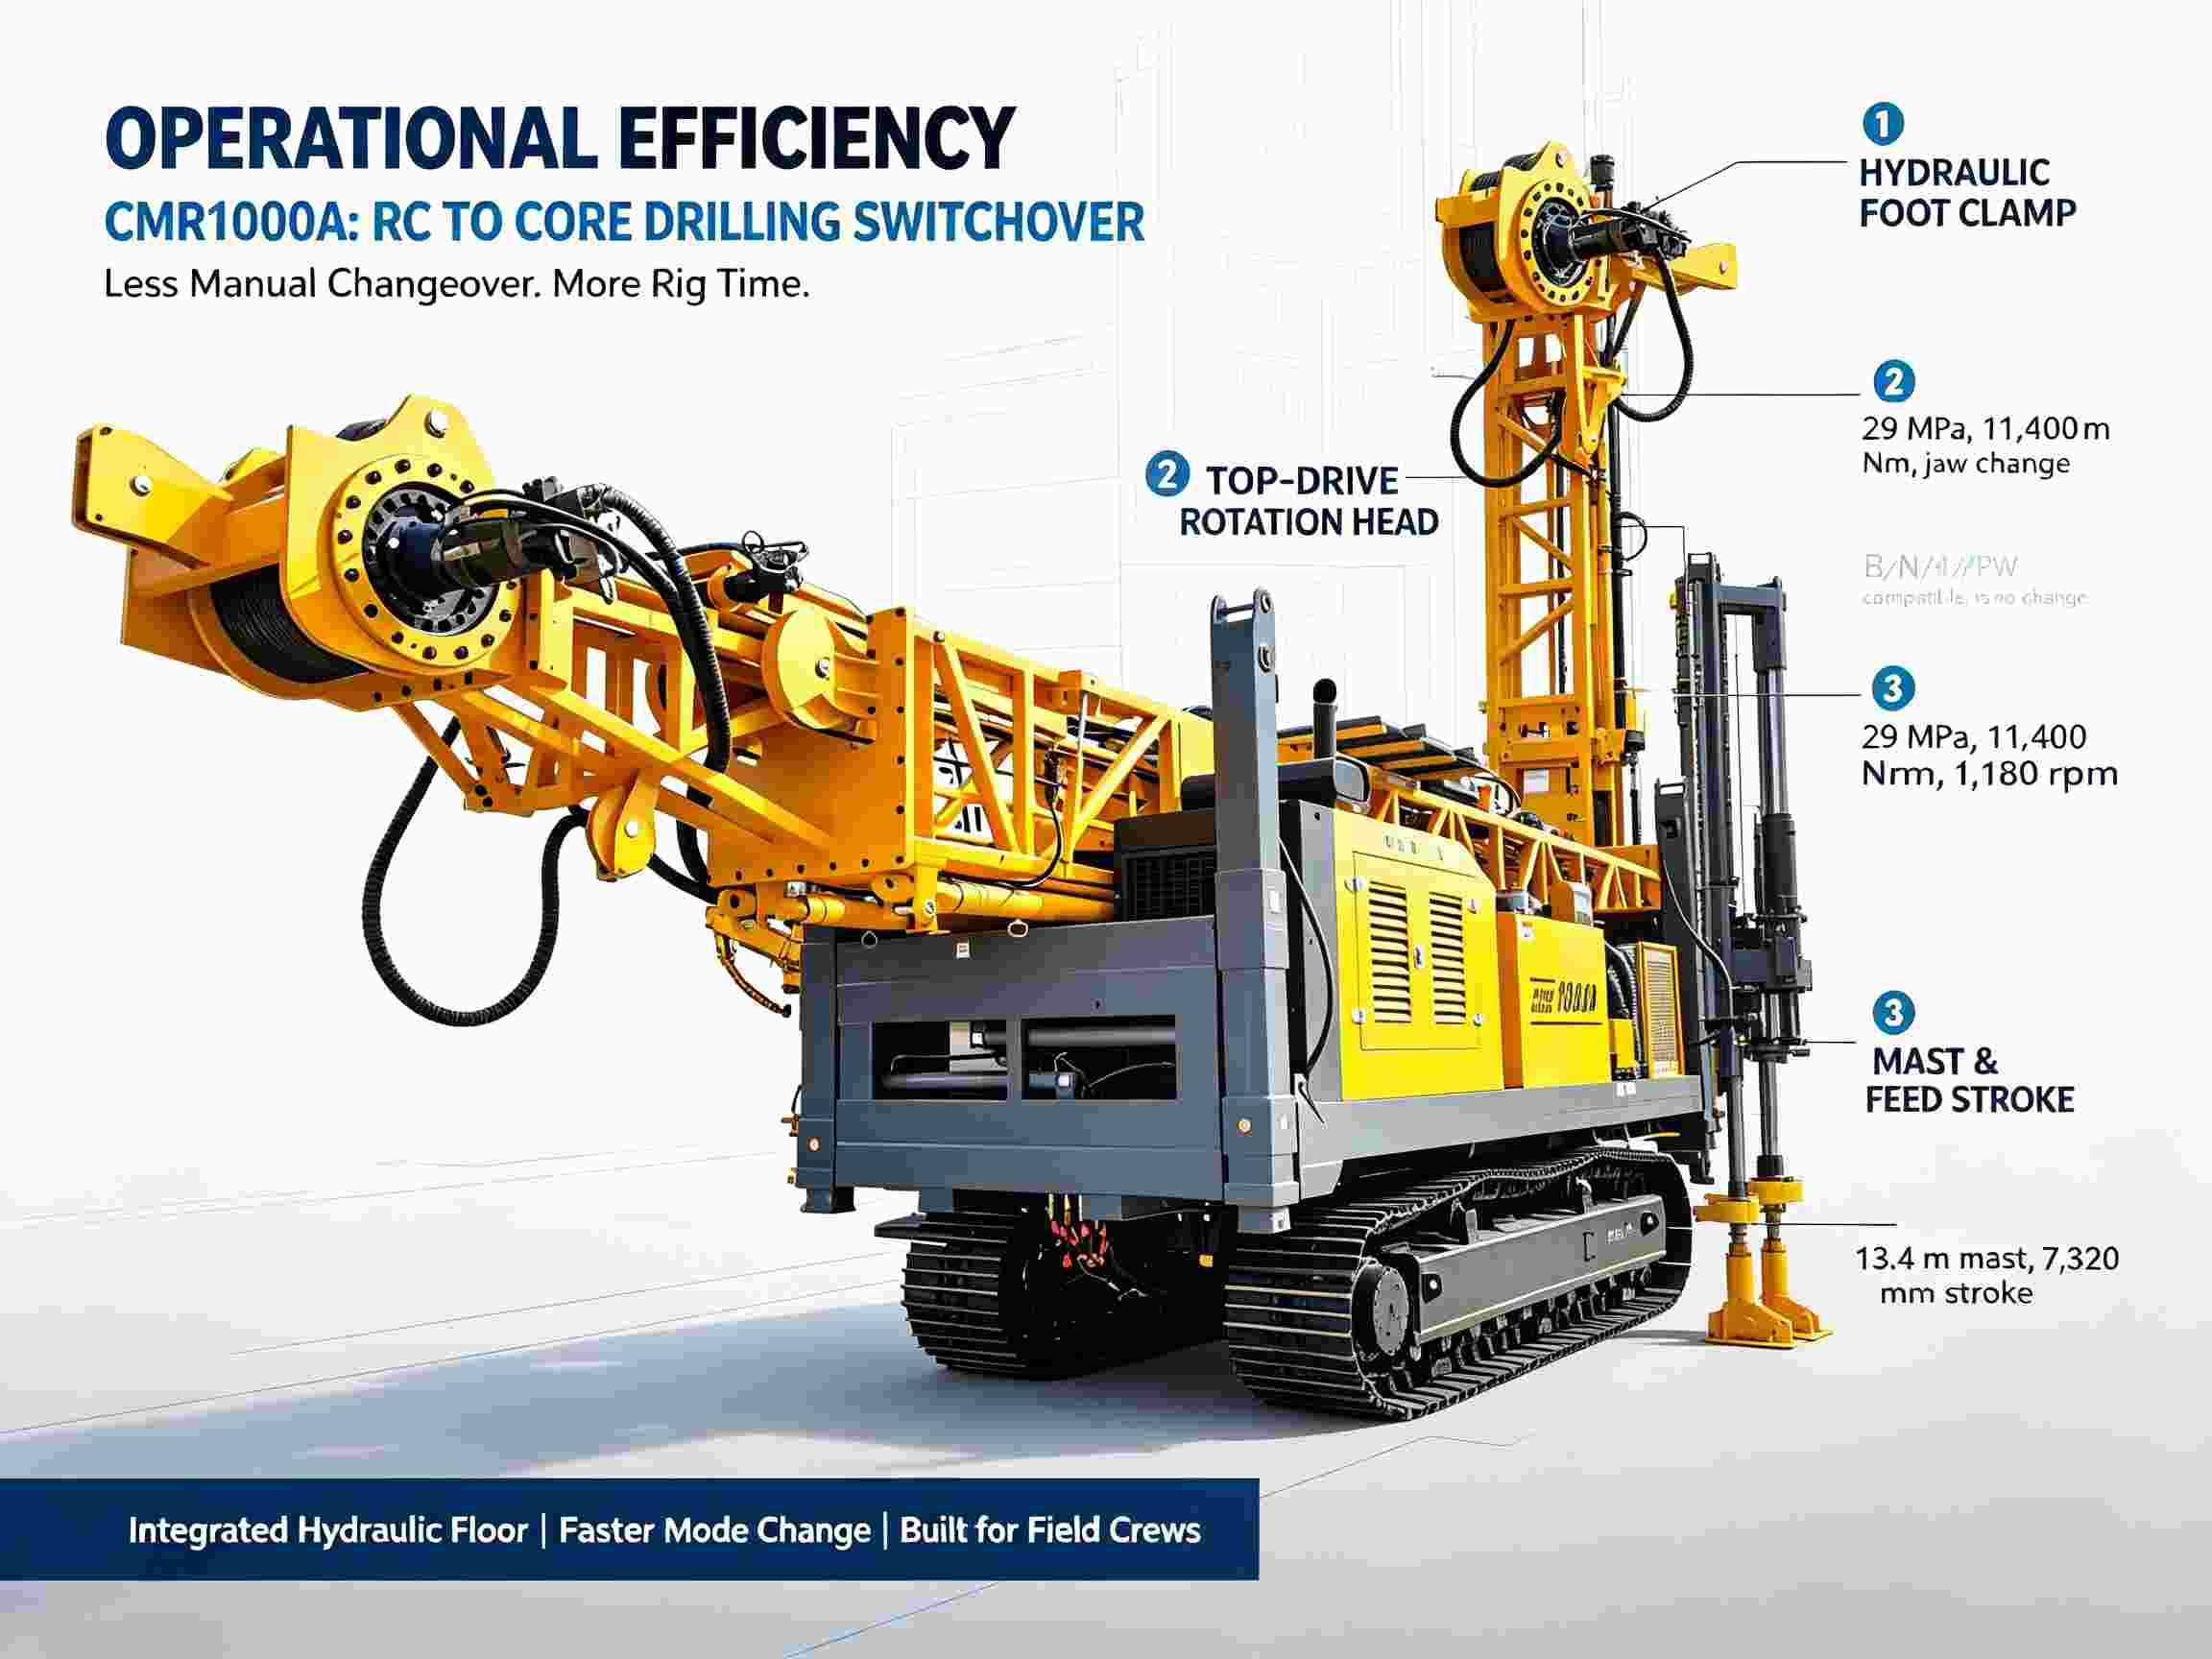
Instead of forcing crews to manually change out the base jaws, the CMR1000A features an advanced, wide-aperture hydraulic foot clamp (Chuck) that natively accommodates B, N, H, P, and PW size drill rods without jaw replacement. Accompanying this is a high-torque hydraulic breakout clamp (Clamp Unloader) factory-calibrated to clamp and break 3.5”, 4”, and 4.5” dual-wall RC rods.When the RC hammer hits the solid target stratum at the bottom of the pre-collar, the driller uses the hydraulic control console to break the final RC joint. The crew lays down the RC string, and the system is immediately ready to accept the diamond core outer tube without a single heavy wrench being swung on the rig floor.
2. Specialized Top-Drive Rotation Head Architecture
A major bottleneck on older hybrid designs was the time spent modifying the rotation head drive subs. The CMR1000A utilizes a high-efficiency top-drive rotation head powered by a robust 29 MPa hydraulic system.With a maximum torque output of 11,400 Nm and a variable speed range peaking at 1,180 rpm, the head can switch gears hydraulically. The driller can transition from high-torque, low-RPM hammer mode to high-RPM, low-torque diamond cutting speed via the control desk, significantly reducing mechanical teardown requirements.
3. Generous Mast Geometry and Slide Stroke
With a full mast height of 13.4 meters and a massive 7,320 mm feed stroke, the CMR1000A easily manages standard long drill strings. Furthermore, the rig features a 1,400 mm mast slide stroke. This allows the entire mast structure to move vertically relative to the borehole, providing excellent clearance for the crew when they are swinging the air cyclone out of alignment and setting up the wireline core pulling system.Reducing the Offsider's Burden in Harsh Climates
Whether operating in the sub-zero winters of the Central Asian steppes or the scorching summer heat of African mining concessions, equipment reliability dictates crew morale and efficiency.The CMR1000A features a rugged all-air-cooling module for its 29 MPa hydraulic system. In remote, water-scarce exploration blocks, traditional water-cooled hydraulics represent a major failure point due to scale build-up or radiator leaks under the aggressive, high-vibration environment of air RC drilling. By relying on a high-capacity air-cooled radiator driven by the 242 kW Cummins engine, the hydraulic fluid maintains optimal viscosity during grueling, continuous operations, saving the crew from unexpected mid-shift breakdown maintenance.
Conclusion: Designed for Drillers, Approved by Management
The CMR1000A multi-functional drilling rig proves that "dual-purpose" doesn't have to mean "double the operational hassle." By automating the heavy-lifting elements of the changeover process through integrated hydraulic chucks, flexible top-drive geometry, and robust all-weather cooling, it respects the physical limits of the field crew while maximizing the project's bottom-line efficiency.Exported worldwide with international CE and ISO certifications by Shanxi Jincheng Anthracite Mining Group International Trading Co., Ltd., the CMR1000A bridges the gap between engineering theory and hard, physical reality on the drill pad.